How to Choose the Best Quality Control Equipment?
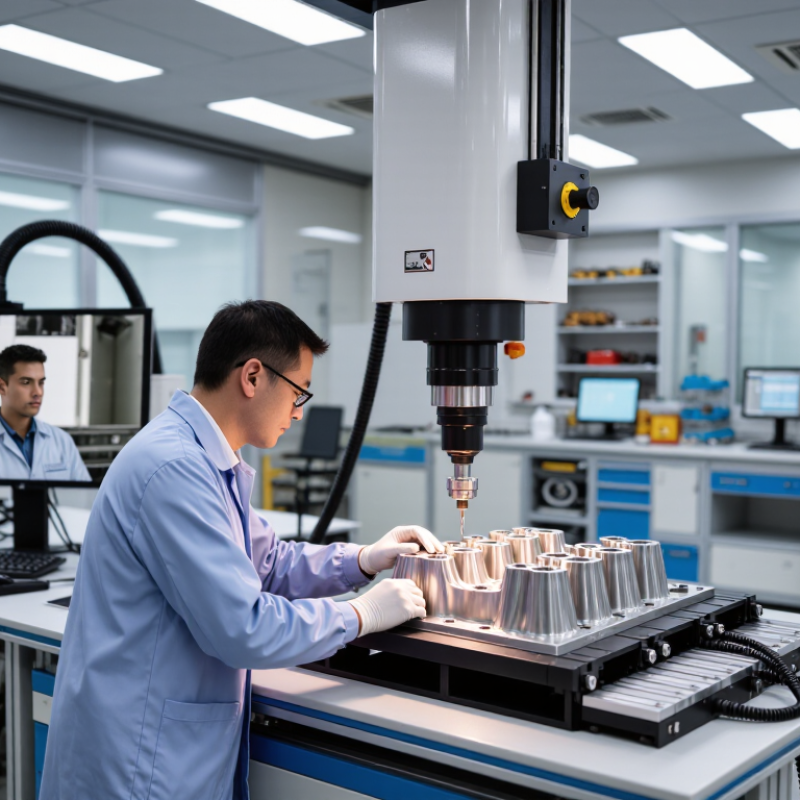
Choosing the best quality control equipment begins with the product, not the catalog. A molded component may need dimensional inspection, surface analysis, or material testing. Each requirement demands a different tool. A camera system can detect scratches quickly. It may miss hidden cracks, however. A coordinate measuring machine can verify tight tolerances. It also requires stable temperature and trained operators.
W. Edwards Deming, a leading quality management expert, said, “Quality comes not from inspection, but from the improvement of the production process.” His point remains practical. Quality control equipment should reveal process problems, not merely reject finished goods. Look for repeatability, calibration support, data traceability, and simple operator controls. Check the equipment beside real production samples. A polished demonstration is not enough.
Small details matter. Can the probe reach narrow cavities? Does the software record calibration dates? Can maintenance teams replace a sensor without stopping production for hours? These questions often separate useful equipment from expensive decoration. Certification and supplier experience also deserve careful review. A reliable vendor should explain measurement uncertainty and provide documented service procedures. Yet no purchase is perfect. Teams may underestimate training time or choose excessive automation. That mistake can create unused equipment beside the production line. The best decision balances accuracy, speed, integration, budget, and future product changes. Start with measurable risks, verify performance under actual conditions, and leave room for honest reassessment.
Define Measurement Needs Using ISO 9001 Risk-Based Quality Criteria
How to Choose the Best Quality Control Equipment?
Define measurement needs before comparing equipment. ISO 9001 supports risk-based thinking, not automatic investment in expensive instruments. Start with product characteristics that could affect safety, performance, fit, or customer satisfaction. A tight dimensional tolerance usually requires better resolution and lower measurement uncertainty. A visible cosmetic feature may need a simpler inspection method.
Quality teams should connect each risk to a measurable requirement. Record the tolerance, expected variation, inspection frequency, environmental conditions, and required data traceability. Temperature, vibration, dust, and operator technique can change results. They should influence equipment selection. Calibration status also matters. Equipment without reliable calibration records can weaken otherwise strong inspection evidence.
Our first risk matrix looked complete, but it ignored operator fatigue during repeated measurements. That was a useful failure. A practical review should include production operators, quality specialists, and maintenance personnel. Ask whether the equipment is easy to use correctly at the actual workstation. Define acceptance rules before purchase. Include resolution, repeatability, reproducibility, calibration intervals, software controls, and training needs. ISO 9001 does not require one specific device. It requires controlled monitoring resources that produce trustworthy results. Small trials can expose problems that a specification sheet hides. A rushed decision may satisfy a checklist but still create uncertain measurements.
Compare Accuracy, Resolution, and Gage R&R with a Target Below 10%
Choosing quality control equipment starts with three questions: How accurate is it, how finely can it measure, and can operators reproduce results?
Accuracy describes closeness to the true value. A device reading 10.02 mm for a certified 10.00 mm standard has a 0.02 mm error.
Resolution is different. It shows the smallest displayed increment, such as 0.001 mm. High resolution cannot repair poor accuracy.
I have seen instruments display impressive decimals while drifting during temperature changes. That detail is easy to miss.
Gage R&R tests the measurement system itself. Repeatability measures variation from the same operator and equipment. Reproducibility compares results between operators.
Calculate study variation against the process tolerance, not only the instrument range. A result below 10% is commonly targeted for capable inspection systems. Between 10% and 30% may require engineering review, depending on risk. Above 30% usually signals unacceptable measurement variation. Set the target before purchasing.
Use calibrated reference standards, multiple parts, and several trained operators. Record measurements under realistic shop conditions.
Warm equipment can behave differently from cold equipment. That matters.
Also check stability over time.
A short Gage R&R study can look excellent, yet a later drift reveals weak control. I would not select equipment from resolution alone. The measurement system must support decisions at the tolerance limit, where small errors become expensive.
Verify Calibration Traceability to SI Units Under ISO/IEC 17025
How to Choose the Best Quality Control Equipment?
Reliable quality control begins with measurement confidence, not a polished equipment display. Choose instruments supported by calibration records linked to SI units through an unbroken traceability chain. This chain should identify reference standards, calibration methods, measurement uncertainty, and each laboratory’s competence. Under ISO/IEC 17025, an accredited laboratory should calibrate equipment within its stated scope. Check the certificate carefully. Confirm the instrument’s serial number, calibration date, environmental conditions, and adjustment results. A certificate can look convincing and still leave questions.
In practical use, I compare the equipment’s accuracy with the product tolerance, not only the advertised resolution. A finer display does not guarantee a better measurement. The calibration certificate should state the uncertainty clearly, because uncertainty affects pass-or-fail decisions. Keep calibration intervals based on risk, usage, drift history, and operating conditions. Fixed annual intervals may be simple, but they are not always appropriate. I once treated a stable instrument like a heavily used one. That choice increased cost without improving control.
Tips: Ask for the laboratory’s current accreditation scope. Verify traceability statements to SI units. Review the decision rule before accepting results. Record temperature, humidity, and handling conditions during critical checks. Do not ignore small details. They often explain large failures. Recheck equipment after impact, repair, or unexplained measurement changes. If documentation feels incomplete, pause the purchase and ask precise questions. Accepting assumptions is tempting, but it weakens reliable quality decisions.
Calculate Three-Year ROI, Maintenance Costs, and Training Requirements
How to Choose the Best Quality Control Equipment?
A low purchase price rarely reveals the real cost of quality control equipment. Calculate a three-year ROI before approving the purchase. Include equipment price, installation, calibration, software, labor, repairs, and downtime. Compare these costs with reduced defects, faster inspections, and fewer customer complaints. A simple calculation is useful: net three-year benefit divided by total three-year cost. Keep the assumptions visible. They may be wrong.
Maintenance details often decide whether equipment remains productive. Ask how frequently sensors need cleaning, calibration, or replacement. Record expected service hours and spare-part costs. A machine requiring weekly adjustment may consume more labor than expected. During evaluations, inspect access panels and test routine cleaning. Small design choices matter. One missed maintenance task can reduce measurement reliability.
Tips: Request a three-year maintenance schedule and training plan before purchase. Estimate training hours for operators, supervisors, and technicians. Include refresher sessions after staff changes. Practical training should cover setup, sample handling, error messages, and recordkeeping. A short pilot can expose hidden difficulties, such as confusing controls or slow reporting. Do not rely only on supplier demonstrations. Have your own operators complete repeated inspections using normal production samples. Their feedback may challenge the original ROI estimate, which is useful before committing resources.
How to Choose the Best Quality Control Equipment?
Three-year ROI, maintenance costs, and operator training requirements for common equipment categories.
Planning model: Three-year ROI is calculated as (three-year measurable benefits − purchase cost − three-year maintenance cost) ÷ purchase cost × 100. The estimates assume stable production volume, 250 operating days per year, and benefits from reduced inspection labor, lower rework, and fewer customer-related defects. Actual results depend on application complexity, utilization, and integration requirements.